Blog
Top 10 Liquid Ring Vacuum Pump Manufacturer in 2026
Liquid ring vacuum pumps are widely used where the gas stream contains moisture, condensable vapor or process liquids that can be difficult for other vacuum technologies to handle.
However, choosing a liquid ring vacuum pump manufacturer involves much more than comparing nominal pumping capacity and purchase price.
Two pumps rated at the same flow may perform very differently once seal liquid temperature, inlet pressure, gas composition and discharge conditions are considered. Manufacturers also differ in their ability to provide two-stage pumps, corrosion-resistant materials, seal liquid recovery systems, condensers, separators and complete engineered vacuum packages.
This guide compares established liquid ring vacuum pump manufacturers based on their current product portfolios, industrial application experience and system capabilities.
It is not a market-share or revenue ranking. The objective is to help industrial buyers identify which manufacturers are most relevant to their process before requesting technical proposals.
For Vacculex models and configurations, see our complete Liquid Ring Vacuum Pump range.
Liquid Ring Vacuum Pump Manufacturers at a Glance
| Manufacturer | Main Strength | Pump / System Capability | Typical Applications |
|---|---|---|---|
| NASH | Heavy-duty liquid ring technology | Single-stage, two-stage, hybrid systems | Power, chemical, paper, oil & gas |
| Busch Vacuum Solutions | Broad DOLPHIN portfolio | Single-stage, two-stage, recirculation systems | Chemical, food, pharmaceutical, general process |
| Atlas Copco | Pumps + engineered systems | Single-stage, two-stage, high-capacity systems | Chemical, distillation, vapor recovery |
| DEKKER | Packaged liquid ring systems | Pumps, water/solvent sealed systems, recovery configurations | Chemical, food, power, general industry |
| Flowserve / SIHI | Process-industry liquid ring pumps | Single-stage, two-stage, engineered packages | Chemical, pharma, energy, process industry |
| Graham | Engineered liquid ring and hybrid systems | Liquid ring, ejector, condenser packages | Petrochemical, power, pharmaceutical |
| Pompetravaini | Broad dedicated liquid ring portfolio | Single-stage, two-stage, large-capacity pumps | Chemical, pharma, industrial process |
| Kenflo | Large industrial liquid ring pumps | Single-stage, two-stage, packaged units | Refinery, chemical, power, large flow |
| Vacculex | Process liquid ring + Roots systems | Single-stage, two-stage, customized systems | Chemical, pharma, wet gas, process vacuum |
A manufacturer should move higher or lower on your shortlist once the actual inlet pressure, gas load, seal liquid temperature and process chemistry are known.
How We Selected These Liquid Ring Vacuum Pump Manufacturers
The manufacturers in this guide were selected because they currently publish dedicated liquid ring vacuum pump products or engineered liquid ring systems.
The comparison considers the depth of the liquid ring product range, availability of single- and two-stage configurations, material options, industrial application coverage and the ability to supply more than a bare pump.
This is important because an industrial liquid ring project often requires more than the rotating machine itself. Depending on the process, the final package may include a separator, heat exchanger, seal liquid circulation, condenser, controls or a Roots booster.
Companies whose main business is vacuum equipment resale, general fluid pumping or repair services have therefore not been included simply to create a longer list.
Leading Liquid Ring Vacuum Pump Manufacturers
NASH is one of the most specialized manufacturers in the liquid ring vacuum market.
Its current portfolio covers medium- and large-capacity liquid ring vacuum pumps as well as dedicated two-stage designs. NASH states that its two-stage AT and TC ranges are intended for lower-pressure industrial service and can also be combined with ejectors or boosters in hybrid systems.
Main Strength
NASH has particularly strong exposure to heavy industrial applications where reliability and wet-gas handling are more important than compact equipment size.
Its published applications include chemical and petrochemical processing, power generation, oil and gas, pulp and paper and other large continuous processes. Material options include cast iron and stainless-steel configurations depending on the pump family and service conditions.
Best Fit / Buyer Note
NASH is especially relevant for large wet-process systems, condenser evacuation and projects that require established liquid ring or hybrid vacuum technology.
When comparing a NASH proposal with another manufacturer, focus on capacity at the actual operating pressure, seal liquid temperature and system configuration rather than nominal pump size alone.
Busch offers a broad liquid ring product family under the DOLPHIN name.
The current DOLPHIN range covers compact pumps, large process pumps and packaged vacuum units. Busch offers both single- and two-stage configurations, along with continuous-flow, partial-recirculation and total-recirculation system arrangements.
Main Strength
One advantage of Busch is the breadth of the DOLPHIN platform. Different series are available for saturated vapor, particle-containing gases, chemical processes and large industrial flow requirements.
Busch also offers multiple materials and, on selected models, alternative operating liquids and configurations for demanding chemical service.
Best Fit / Buyer Note
Busch is worth evaluating when the project requires a globally supported liquid ring platform with multiple pump sizes and system options.
Buyers should still determine whether the process is better suited to a single-stage or two-stage DOLPHIN and whether once-through or recirculated seal liquid is more appropriate.
Atlas Copco currently offers a substantial liquid ring portfolio built around its AWS, AWD, AWL and related ranges.
Its engineered liquid ring systems include single- and two-stage configurations and cover capacities from small process duties to very large industrial flow requirements. Atlas Copco specifically positions these systems for applications such as vapor recovery, degassing, distillation and other complex process duties.
Main Strength
Atlas Copco combines standalone pumps with engineered system capability.
Its AWS single-stage range, for example, can be configured with different materials and recovery arrangements, while the AWD platform provides two-stage operation for lower-pressure duties.
Best Fit / Buyer Note
Atlas Copco is particularly relevant when the project requires an engineered package rather than simply a replacement pump.
When comparing proposals, look closely at the proposed seal liquid circuit, cooling system, controls and expected performance at your real water temperature.

DEKKER offers dedicated liquid ring pumps as well as several packaged liquid ring vacuum system families.
Its current portfolio includes Titan and Maxima liquid ring pumps together with AquaSeal water-sealed systems, ChemSeal solvent-sealed systems and Vmax oil-sealed liquid ring systems.
Main Strength
DEKKER is especially strong in packaged system configurations.
Its AquaSeal systems can use single- or two-stage pumps and can be configured for once-through, partial-recovery or full-recovery operation. The systems can also be built using different materials for corrosive or difficult gas streams.
Best Fit / Buyer Note
DEKKER is worth considering where seal liquid consumption, solvent compatibility or packaged system design is a major part of the project.
For applications such as solvent recovery or vacuum distillation, compare the complete liquid management arrangement rather than just the pump.
SIHI is Flowserve’s process-vacuum brand and offers liquid ring pumps designed for industrial process applications.
The current SIHI liquid ring portfolio includes products such as the LEMD and LPH ranges. The LPH platform includes single- and two-stage between-bearing configurations and is supported by engineered and pre-engineered vacuum packages.
Main Strength
Flowserve / SIHI has strong relevance to process industries where pumps, materials and vacuum systems must integrate with broader plant requirements.
SIHI equipment is used across chemical processing, pharmaceuticals, food and beverage, energy and general industrial applications.
Best Fit / Buyer Note
SIHI is particularly relevant for buyers that already use process equipment standards associated with large chemical or industrial plants.
Ask whether the quoted model is a standalone liquid ring pump or part of a broader engineered system, and confirm the material specification for the actual gas and operating liquid.
Graham combines liquid ring vacuum pumps with condensers, steam ejectors and complete vacuum systems.
Its liquid ring pumps are available in different materials and can operate with service liquids other than water where the process requires it. Graham also produces two-stage liquid ring arrangements for applications such as power-generation condenser evacuation.
Main Strength
Graham’s key differentiator is system engineering around the pump.
The company combines liquid ring vacuum pumps with ejectors, condensers and other process equipment for petrochemical, power-generation and pharmaceutical duties.
Best Fit / Buyer Note
Graham is particularly relevant when a liquid ring pump forms part of a larger process vacuum package.
For refinery or vacuum distillation projects, buyers should compare the complete system operating cost and suction performance rather than treating the vacuum pump as an isolated component.
Pompetravaini
Pompetravaini maintains a broad portfolio dedicated to liquid ring vacuum technology.
Its current product range includes multiple single-stage series, dedicated double-stage TRH pumps and large-capacity TRVK / TRSK designs. Published capacities extend from compact close-coupled units to large industrial pumps.
Main Strength
The depth of the liquid ring range allows Pompetravaini to cover both standard industrial vacuum and more specialized applications.
Its two-stage TRH series is available for higher-vacuum applications and can also be supplied in special materials for process compatibility.
Best Fit / Buyer Note
Pompetravaini is worth evaluating when a project requires a dedicated liquid ring manufacturer with multiple frame sizes and material configurations.
As with any liquid ring supplier, make sure the performance curve is evaluated using the intended operating liquid and temperature.
Kenflo is a Chinese pump manufacturer with a substantial dedicated liquid ring portfolio.
Its current product range includes 2BE1, CBF, CDF, SK and CBE2 liquid ring pumps together with liquid ring compressors and packaged vacuum units.
Main Strength
Kenflo covers a particularly wide flow range.
Its CBE2 series provides two-stage operation, while its large CBF and 2BE1 families address high-capacity industrial applications. Material options published for selected ranges include cast materials, several stainless-steel grades, duplex stainless steel and special alloys.
Best Fit / Buyer Note
Kenflo is relevant for chemical, refining, power and other industrial projects where large flow or customized materials are required.
For international sourcing, buyers should confirm motor standards, instrumentation, documentation, system scope and after-sales support together with the pump specification.

Vacculex is a China-based industrial vacuum manufacturer offering several Liquid Ring Vacuum Pump families including VLRC, B, KLRPV and KLRPE.
The portfolio covers both standard process pumps and lower-pressure two-stage configurations, while customized systems can combine liquid ring pumps with Roots boosters when higher pumping capacity is required at lower pressure.
Main Strength
Vacculex focuses on process vacuum applications involving wet gases, condensable vapor and industrial system requirements.
The VLRC Two-Stage Liquid Ring Vacuum Pump is designed for moist mixed gases and small quantities of entrained liquid, with two-stage compression for demanding lower-pressure applications.
For applications requiring greater pumping capacity at lower pressure, Vacculex also supplies a dedicated Roots and Liquid Ring Vacuum System for applications including chemical processing, pharmaceuticals, drying and vapor recovery.
Best Fit / Buyer Note
Vacculex is most relevant to industrial buyers looking for a liquid ring pump or customized process vacuum system rather than a small general-purpose pump.
The selection should begin with the required inlet pressure, pumping speed, gas composition and seal liquid condition.
Comparing Liquid Ring Vacuum Pump Manufacturers?
Send Vacculex your required inlet pressure, pumping speed, gas composition and seal liquid temperature.
We can help determine whether a single-stage, two-stage or Roots + liquid ring configuration is more appropriate for your process.
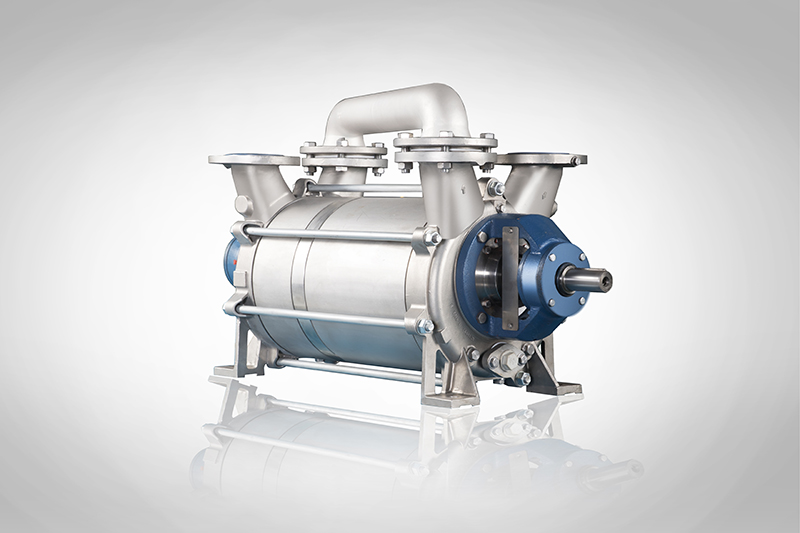
How to Compare Liquid Ring Vacuum Pump Manufacturers
The best manufacturer is not necessarily the company with the largest pump or the lowest quotation.
A useful comparison should focus on how well the proposed pump performs under the actual process conditions.
Single-Stage vs Two-Stage Capability
Single-stage liquid ring pumps are widely used for moderate industrial vacuum and high gas-flow duties. Two-stage pumps divide compression between two stages and are generally more suitable where lower operating pressure is required.
Manufacturers such as NASH, Busch, Atlas Copco, Flowserve/SIHI and Pompetravaini all offer dedicated two-stage configurations. Vacculex provides the VLRC two-stage series for lower-pressure process duties.
The decision should not be based on stage count alone. Gas load, operating liquid, required pressure and power consumption must be evaluated together.
For a detailed technical comparison, see Single-Stage vs Two-Stage Vacuum Pumps.
Performance at the Actual Seal Liquid Temperature
Seal liquid temperature directly affects liquid ring vacuum pump performance because the vapor pressure of the operating liquid influences the achievable inlet pressure.
A performance curve based on cooler water can therefore overstate the capacity available in a plant using warmer seal water.
When comparing manufacturers, ask for pumping speed at:
your required inlet pressure + actual seal liquid temperature + expected gas conditions.
Do not compare two pumps only from their nominal m³/h or CFM rating.
This becomes particularly important in summer operation, closed-loop systems and processes where the circulating liquid absorbs significant heat.
Materials and Gas Compatibility
Liquid ring pumps are often selected precisely because they must handle difficult gases.
The pump material, mechanical seals and operating liquid therefore need to be compatible with the process.
Manufacturers may offer combinations of cast iron, stainless steel, duplex materials and, for specialized duties, more corrosion-resistant alloys. Busch, Graham, Kenflo and Pompetravaini all publish multiple material options for different process conditions.
For chemical projects, provide the actual gas composition rather than simply stating that the pump will handle “chemical vapor.”
Seal Liquid Recovery Design
Water consumption can be a major operating cost in a liquid ring system.
Three common arrangements are once-through, partial recirculation and full recirculation.
Once-through systems are simple but consume more fresh liquid. Partial recovery reuses part of the discharged liquid, while full-recovery systems separate, cool and return most of the operating liquid to the pump.
DEKKER’s AquaSeal systems and Busch’s DOLPHIN packaged units are examples of manufacturers offering multiple recovery configurations.
The correct design depends on process contamination, cooling capacity, water availability and discharge requirements.
System Engineering Capability
Many industrial applications require more than a liquid ring pump.
The system may also need a gas-liquid separator, heat exchanger, condenser, control valves, instrumentation or a Roots booster.
This is where two manufacturers quoting similar pump capacities can provide very different solutions.
For lower-pressure or higher-capacity applications, Vacculex can combine a Roots Vacuum Pump with a liquid ring backing pump as part of a Customized Vacuum System.
System capability becomes especially important for distillation, evaporation, vapor recovery and large continuous processes.
Which Liquid Ring Vacuum Pump Manufacturer Fits Your Application?
Different industries place different demands on the pump. The following groups are a practical starting point, not an absolute ranking.
Chemical and Petrochemical Processing
Chemical processes may involve corrosive gases, solvents, condensable vapor and fluctuating loads.
Manufacturers worth comparing include NASH, Busch, Atlas Copco, Flowserve/SIHI, Graham and Vacculex because each offers liquid ring technology or engineered systems relevant to process vacuum.
The most important comparison is normally material compatibility, operating liquid selection and performance at the real process pressure.
Power Generation
Power applications frequently use liquid ring pumps for condenser evacuation and related vacuum duties.
NASH and Graham both publish dedicated equipment for power-generation service, while Atlas Copco, Kenflo and other large industrial liquid ring suppliers can also support high-flow vacuum requirements.
Reliability, capacity under condenser conditions and continuous operation are generally more important than achieving the lowest possible nominal ultimate pressure.
Pulp and Paper
Liquid ring pumps have a long history in pulp and paper because the process frequently involves large volumes of wet gas and water.
NASH has particularly strong specialization in this sector, while Busch and Atlas Copco also provide industrial liquid ring platforms suitable for wet process conditions.
Large-flow capability and water-management strategy should be evaluated carefully because the operating cost of the seal liquid system can become significant.
Vacuum Distillation and Solvent Recovery
These applications can place simultaneous demands on vacuum level, vapor handling, corrosion resistance and condensation management.
DEKKER provides water- and solvent-sealed system options, while Graham combines liquid ring pumps with condensers and ejectors. Atlas Copco and Vacculex also provide engineered configurations for process vacuum and vapor-handling duties.
For these applications, evaluate the condenser and seal liquid system together with the vacuum pump.
Wet Gas and Condensable Vapor
Liquid ring technology is particularly attractive when moisture or condensable vapor is inherent to the process.
Busch describes its DOLPHIN range as suitable for saturated gases and vapors, while Atlas Copco specifically positions liquid ring pumps for wet gas and liquid carryover. Vacculex’s VLRC series is designed for moist mixed gases and small entrained droplets.
The correct manufacturer should be selected according to the gas chemistry, required pressure and expected liquid load.
Liquid Ring Manufacturer Comparison by Application
| Application | Manufacturers Worth Comparing |
| Chemical processing | NASH, Busch, Atlas Copco, Flowserve/SIHI, Graham, Vacculex |
| Petrochemical / refinery | NASH, Graham, Flowserve/SIHI, Busch |
| Pulp & paper | NASH, Busch, Atlas Copco |
| Power generation | NASH, Graham, Atlas Copco, Kenflo |
| Vacuum distillation | Graham, DEKKER, Atlas Copco, Vacculex |
| Solvent recovery | DEKKER, Graham, Busch, Vacculex |
| Wet gas / condensable vapor | NASH, Busch, Atlas Copco, Vacculex |
| Large-flow process vacuum | NASH, Busch, Atlas Copco, Kenflo, Pompetravaini |
| Customized vacuum system | Atlas Copco, DEKKER, Graham, Vacculex |
The final shortlist should be narrowed using actual operating data rather than industry name alone.
Which Liquid Ring Pump Configuration Should You Choose?
Single-Stage Liquid Ring Vacuum Pump
A single-stage pump is often appropriate when the process requires moderate vacuum, relatively high gas flow and reliable handling of wet gases.
It usually has a simpler configuration and can be a practical choice for general process vacuum, filtration, dewatering and many industrial extraction duties.
The operating point should still be checked against the manufacturer’s curve at the actual seal liquid temperature.
Two-Stage Liquid Ring Vacuum Pump
A two-stage design becomes more relevant when the required inlet pressure is lower and a single-stage pump would be operating close to its practical vacuum limit.
Dividing compression between two stages can improve operation at lower pressure and reduce the compression burden on each stage.
Vacculex’s VLRC Two-Stage Liquid Ring Vacuum Pump is one option for wet and condensable process gases requiring lower-pressure performance.
For a deeper comparison, see Single-Stage vs Two-Stage Vacuum Pumps.
Roots + Liquid Ring Vacuum System
Where the process requires significantly higher pumping speed at lower pressure, adding a Roots booster may be more effective than simply installing a larger liquid ring pump.
The Roots pump increases pumping capacity in its working pressure range while the liquid ring pump provides the backing vacuum and handles the wet gas stream.
Vacculex’s Roots and Liquid Ring Vacuum System is designed around this configuration for applications including chemical processing, pharmaceutical production, drying and vapor recovery.
The booster and backing pump must be sized as one coordinated system.
After Selecting the Manufacturer: Reliability Still Depends on Operation
Even a correctly selected liquid ring vacuum pump can lose capacity if seal liquid temperature rises, the suction system leaks or cavitation develops.
For diagnosing an existing system, see our Liquid Ring Vacuum Pump Troubleshooting Guide.
For preventive inspection and routine servicing, see Liquid Ring Vacuum Pump Maintenance.
These operating factors should also be considered when comparing manufacturers because the quality of technical documentation and after-sales support affects long-term reliability.
Frequently Asked Questions
Who Are the Leading Liquid Ring Vacuum Pump Manufacturers?
Established liquid ring manufacturers include NASH, Busch, Atlas Copco, DEKKER, Flowserve/SIHI, Graham, Pompetravaini, Kenflo and Vacculex.
They serve different parts of the market, so there is no single best manufacturer for every application.
How Do I Choose a Liquid Ring Vacuum Pump Manufacturer?
Start with the required inlet pressure, pumping speed, gas composition and seal liquid temperature.
Then compare manufacturers according to single- or two-stage capability, materials, performance curves, recirculation design and system engineering.
Price should be compared only after the technical configuration is equivalent.
Which Manufacturers Offer Two-Stage Liquid Ring Vacuum Pumps?
Manufacturers with current two-stage product or system options include NASH, Busch, Atlas Copco, Flowserve/SIHI, Graham, Pompetravaini, Kenflo and Vacculex.
The correct choice still depends on required pressure and process conditions.
What Should I Compare Besides Pumping Capacity?
Compare actual capacity at the required pressure, seal liquid temperature, materials, motor power, discharge-pressure capability, system configuration and after-sales support.
Two pumps with the same nominal m³/h rating may perform differently under the same plant conditions.
Conclusion
Choosing a liquid ring vacuum pump manufacturer should not begin with a list of prices.
A more reliable selection process is:
Define the Operating Pressure → Confirm Gas and Vapor Conditions → Select Single- or Two-Stage Technology → Compare Performance at the Actual Seal Liquid Temperature → Evaluate Materials and Recovery System → Compare Complete System Capability
NASH, Busch, Atlas Copco, DEKKER, Flowserve/SIHI, Graham, Pompetravaini, Kenflo and Vacculex all offer legitimate liquid ring technologies, but their strengths differ.
The right manufacturer is the one whose pump and system configuration best match the real operating conditions.
For industrial wet-gas, condensable-vapor or customized process applications, explore Vacculex Liquid Ring Vacuum Pumps or send your operating data for an application-based recommendation.